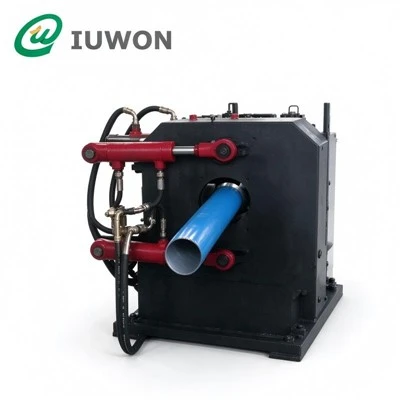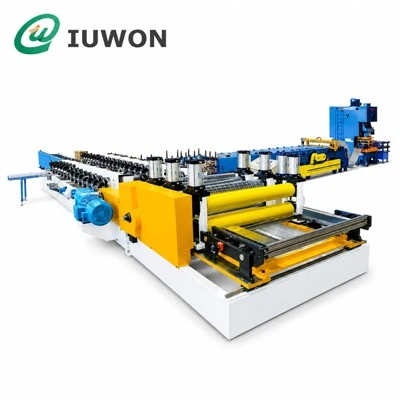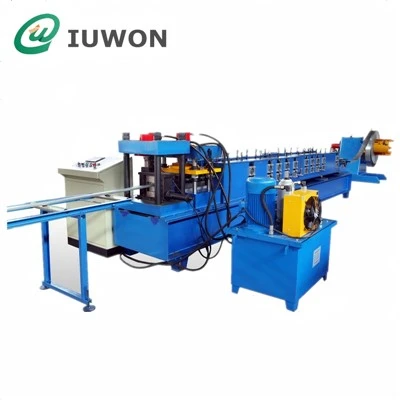
Hangzhou IUWON Technology Co., Ltd. is one of the most reliable manufacturers and suppliers of downspout roll former in China. With abundant experience, we warmly welcome you to buy custom made downspout roll former from our factory. Good service and reasonable price are available.
Downspout Roll Former Specifications
| Forming Method | Cold Roll Forming |
| Product Profiles | Round, square, rectangular, customized |
| Suitable Materials | Galvanized steel, pre-painted steel, aluminum, subject to confirmation |
| Material Thickness | 0.4–0.7 mm for applicable round downspout configurations |
| Forming Speed | Approximately 10–15 m/min, depending on configuration |
| Forming System | Multi-station roller tooling |
| Cutting Method | Hydraulic post-cutting for the referenced configuration |
| Control System | PLC control |
| Length Measurement | Encoder-based measurement, subject to configuration |
| Pipe Dimensions | Customized according to approved drawings |
| Electrical Supply | Confirmed according to destination-country requirements |
These are reference specifications for applicable configurations, not guaranteed values for every machine. Final material thickness, speed, motor power, cutting tolerance, dimensions, and included functions must be confirmed in the technical quotation.
Downspout Profiles and Sizes
The finished pipe design determines the roller geometry and forming arrangement. Different cross-sections require different tooling considerations, so the required dimensions should be confirmed before manufacturing the machine.
| Profile Type | Main Specifications to Confirm |
|---|---|
| Round downspout | Pipe diameter, seam design, and connection dimensions |
| Square downspout | Side length, corner shape, and joint position |
| Rectangular downspout | Width, depth, corner geometry, and installation clearance |
| Custom profile | Cross-section drawing, edge details, and fitting requirements |
If several sizes are required, IUWON can evaluate whether the proposed machine should use dedicated tooling, interchangeable tooling, or another configuration. The available size range and changeover method depend on the specific design.
Roll Forming Process
The production process begins with a metal coil and ends with downpipes cut to the required length.
- Coil feeding: The metal strip is supplied to the forming section through the selected decoiling and guiding arrangement.
- Progressive forming: Successive roller stations gradually shape the strip into the specified cross-section.
- Profile sizing: The forming arrangement establishes the required pipe geometry and prepares the edges for the intended joint.
- Joint formation: The strip edges are brought together according to the approved pipe construction.
- Length cutting: The formed pipe is cut according to the required product length.
- Finished-product inspection: Operators check dimensions, seam condition, surface appearance, and cut ends against the agreed requirements.
The forming sequence and tooling must be designed for the actual profile. Correct roller alignment and gradual deformation help limit profile distortion and inconsistent dimensions.
Cutting System
The cutting arrangement affects production rhythm, finished length, and the way operators handle completed pipes.
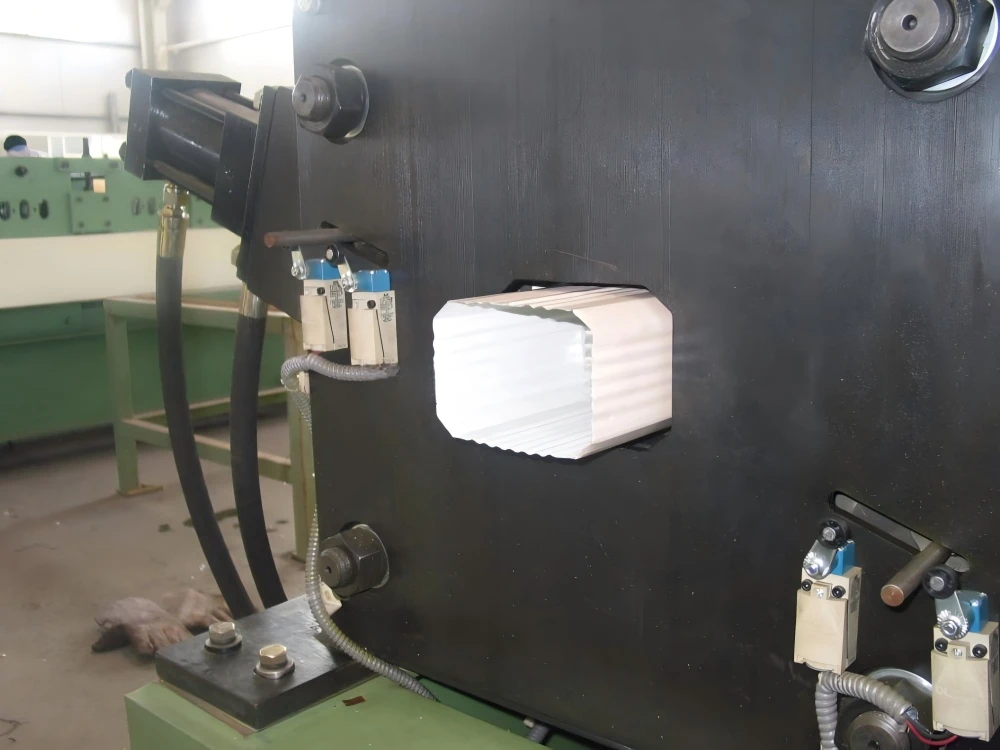
Hydraulic post-cutting can be used for suitable machine configurations. If higher throughput or continuous movement is required, an alternative synchronized cutting arrangement can be evaluated where supported by the machine design.
Before placing an order, confirm the following:
- Standard and maximum finished pipe lengths.
- Required cutting-length tolerance.
- Whether the line stops during cutting.
- Required condition of the cut edges.
- Finished-pipe support and collection method.
Actual output depends on the cutting cycle and handling process as well as nominal forming speed. The production target should therefore be confirmed using the intended material, profile, and finished length.
Downspout Roll Former Configuration
The machine configuration should reflect the manufacturer's production requirements and factory conditions.
| Configuration Item | What to Confirm |
|---|---|
| Roller tooling | Profile dimensions and number of sizes required |
| Feeding system | Coil dimensions and loading method |
| Control system | Required operating and length-setting functions |
| Cutting unit | Cutting method and required tolerance |
| Electrical system | Local voltage and frequency |
| Discharge area | Maximum pipe length and collection arrangement |
| Safety provisions | Guarding, emergency stops, and operator access |
For factories manufacturing one standard pipe size in large batches, a dedicated configuration may be appropriate. Manufacturers handling multiple sizes should evaluate tooling changes, setup time, and the cost of producing different profiles before selecting the final arrangement.
Applications
Residential roofing
Downpipes for houses, villas, and residential developments.
01
Commercial buildings
Rainwater drainage components for offices, retail buildings, and other commercial properties.
02
Industrial facilities
Metal downpipes for factory buildings, warehouses, and workshops.
03
Roofing-material suppliers
Standard pipe sizes supplied to contractors and distributors.
04
Customized building projects
Profile-specific downpipes manufactured according to approved drawings.
05
The required profile, material, and dimensions should be determined by the building design and the customer's specifications.
FAQ
Can the machine produce different downspout sizes?
This depends on the machine design and tooling arrangement. Specify all required dimensions before ordering so the available size range and changeover method can be confirmed.
What is the maximum forming speed?
The reference speed for applicable round downspout configurations is approximately 10–15 m/min. Actual operating speed depends on the selected machine, material, profile, and cutting arrangement.
Can pre-painted steel be processed?
Pre-painted steel can be considered for suitable configurations. Material thickness, coating condition, roller surfaces, and handling requirements should be reviewed before the machine is finalized.
Can the finished pipe length be adjusted?
The cutting and control configuration can be selected according to the required lengths. The available adjustment functions and achievable cutting tolerance must be specified in the technical offer.
What information is needed for a quotation?
Provide the pipe drawing or sample, material type, thickness, required dimensions, finished lengths, target output, destination country, and factory power supply.
Request a Quotation
To select a suitable downspout roll former, send IUWON your required pipe profile, material specifications, target production volume, and finished lengths.
The engineering team can evaluate the forming tooling, cutting arrangement, control system, and auxiliary equipment required for your application. Final machine specifications can then be confirmed against your approved drawings and operating requirements.
Contact IUWON to discuss your downspout production requirements.
Customize Your Downspout Roll Former
Hot Tags: downspout roll former, China downspout roll former manufacturers, suppliers, factory, down pipe roll forming machine, pipe forming machine for rainwater drainage, roof water drainage pipe forming line, round downpipe roll forming machine, round tube rainwater pipe machine, steel downpipe forming line