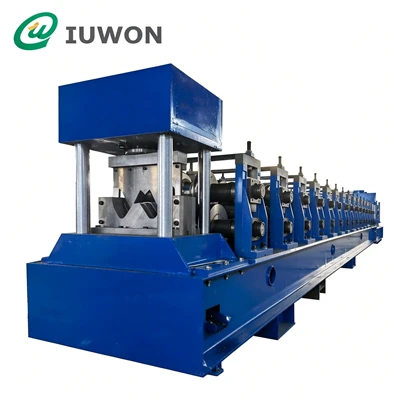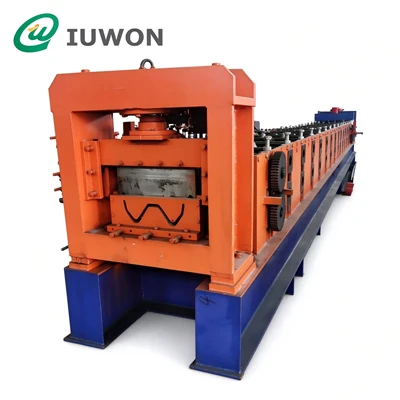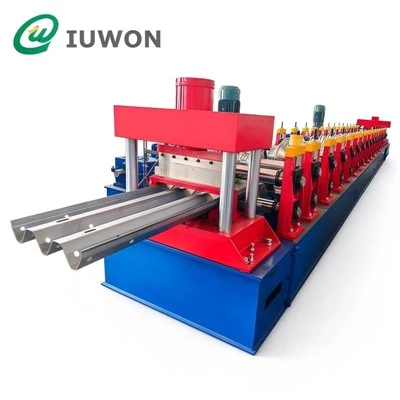
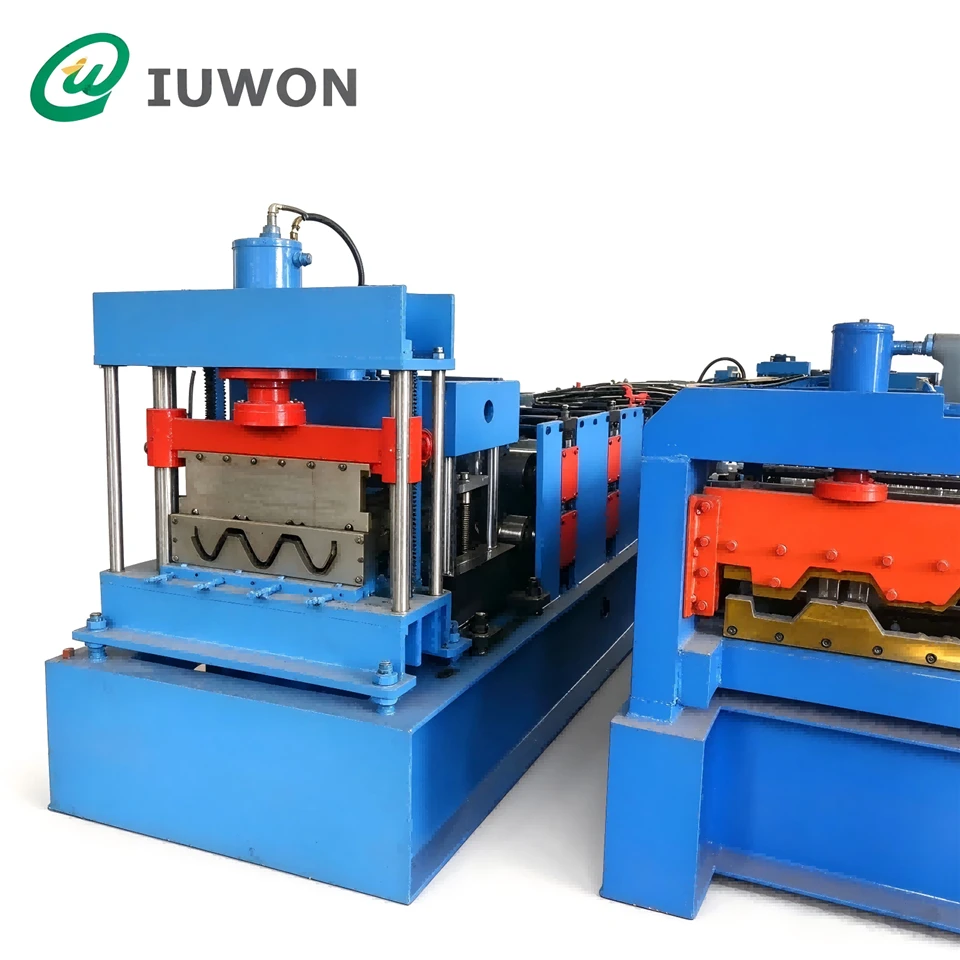
Hangzhou IUWON Technology Co., Ltd. is one of the most reliable manufacturers and suppliers of guardrail roll former in China. With abundant experience, we warmly welcome you to buy custom made guardrail roll former from our factory. Good service and reasonable price are available.
Guardrail Roll Former Parameters
The following reference specifications are published for IUWON guardrail equipment. Confirm the final values for your selected model before ordering.
|
Parameter |
Reference Specification |
|---|---|
|
Product profile |
Two-wave W-beam / three-wave Thrie-beam |
|
Material |
Galvanized steel / carbon steel |
|
Material thickness |
2.5–4.0 mm |
|
Coil width |
According to the approved beam profile |
|
Forming speed |
8–12 m/min |
|
Forming stations |
18–24 |
|
Shaft diameter |
80–95 mm |
|
Shaft material |
40Cr |
|
Roller material |
GCr15 / 45# steel |
|
Main motor power |
22–30 kW |
|
Transmission |
Gearbox + universal joint |
|
Punching |
Hydraulic / servo, subject to configuration |
|
Cutting |
Hydraulic cut-off |
|
Control system |
PLC + touchscreen |
|
Length measurement |
Encoder |
|
Electrical supply |
380 V / 50 Hz / 3-phase |
Profile Options
|
Profile |
Production Considerations |
|---|---|
|
W-beam |
Two-wave cross-section, beam width, mounting holes, and joint geometry |
|
Thrie-beam |
Three-wave cross-section, forming sequence, and dedicated tooling |
|
Custom guardrail |
Profile drawing, material properties, and project-specific dimensions |
Different road projects may specify different beam dimensions and connection details. Before tooling design, provide the approved cross-section drawing and the applicable project standard.
Guardrail Roll Former Tooling
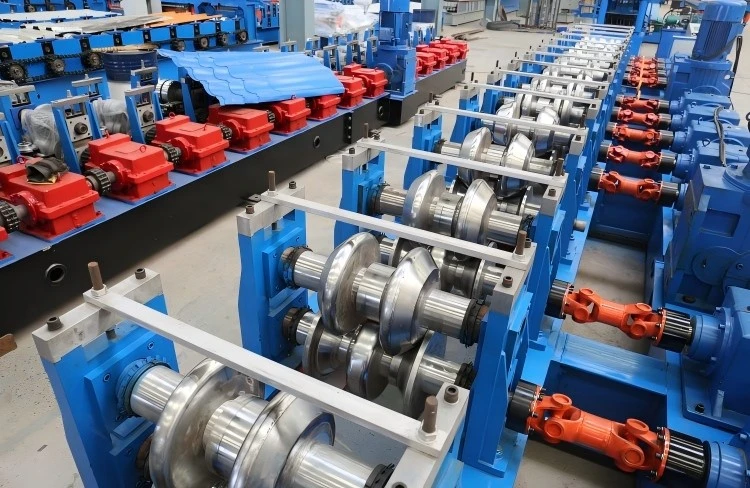
The roller tooling determines the finished guardrail geometry. Each forming station gradually shapes the steel strip, distributing deformation across the profile rather than creating the entire cross-section in one operation.
When reviewing the tooling design, confirm:
- Roller dimensions match the approved profile drawing.
- The forming sequence suits the specified steel thickness and grade.
- The shaft and drive configuration meet the required forming load.
- Roller surfaces are suitable for the material and finish requirements.
- Tooling changes are clearly defined if multiple profiles are required.
For manufacturers supplying several guardrail specifications, the choice between dedicated tooling and interchangeable tooling should be based on order volume, changeover time, and investment budget.
Punching and Cutting
Guardrail beams require mounting holes that align with posts, spacers, and connecting hardware. Hole positions must therefore be controlled according to the approved drawing.
The production line can incorporate a punching unit and a hydraulic cutting system. The punching arrangement should be selected according to the hole diameter, pitch, quantity, and position. The cutting system should match the required finished length and tolerance.
Before confirming the machine, specify:
|
Requirement |
Details to Confirm |
|---|---|
|
Hole dimensions |
Diameter, slot dimensions, and tolerance |
|
Hole positions |
Pitch and distance from profile edges |
|
Punching method |
Hydraulic or servo-controlled, as applicable |
|
Finished length |
Standard and customized lengths |
|
Length tolerance |
Project acceptance requirement |
|
Discharge |
Run-out table or stacking arrangement |
Material Requirements
Steel grade and thickness affect the forming load, tooling design, and final profile. The supplier should evaluate these properties before confirming the machine configuration.
|
Material Information |
Why It Matters |
|---|---|
|
Steel grade |
Determines the material's mechanical properties |
|
Thickness range |
Affects forming force and equipment sizing |
|
Yield strength |
Helps establish forming requirements |
|
Coil width |
Must match the developed strip width |
|
Coil weight |
Determines decoiler capacity |
|
Surface coating |
Influences surface protection and handling |
Do not assume that a machine rated for one thickness can process every steel grade within that range. Provide the material specifications so the proposed configuration can be checked against actual production conditions.
Guardrail Roll Former Capacity
The right machine should match the factory's expected order volume, not just its maximum forming speed.
Production planning should account for the time required to load coils, change tooling, punch holes, cut beams, inspect finished products, and move them to storage.
Before purchasing, establish:
- Required finished beams per shift
- Number of profiles and thicknesses
- Standard beam lengths
- Available operating hours
- Changeover frequency
- Finished-product handling arrangements
Ask for an estimated finished output based on your actual profile and material. This allows a more meaningful comparison between equipment offers and helps identify whether additional handling equipment is needed.
Line Configuration
A typical production line may include the following units:
|
Equipment |
Function |
|---|---|
|
Hydraulic decoiler |
Supports and feeds the steel coil |
|
Leveling unit |
Reduces coil curvature |
|
Feeding and guiding system |
Positions the strip for processing |
|
Punching unit |
Creates the specified mounting holes |
|
Roll forming unit |
Forms the guardrail cross-section |
|
Hydraulic cutting unit |
Cuts the beam to the required length |
|
Run-out table |
Supports finished beams after cutting |
|
PLC control system |
Coordinates machine operation |
The final equipment list depends on the project. Confirm whether coil loading equipment, automatic stacking, additional tooling, installation, and commissioning are included in the quotation.
Quality Inspection
Machine acceptance should be based on the finished guardrail rather than equipment operation alone.
|
Inspection Item |
Acceptance Basis |
|---|---|
|
Cross-section |
Approved profile drawing |
|
Beam dimensions |
Agreed dimensional tolerances |
|
Hole layout |
Approved punching drawing |
|
Finished length |
Specified length tolerance |
|
Surface condition |
Agreed coating and appearance requirements |
|
Connection fit |
Compatibility with posts and joining components |
For projects governed by a road safety standard, confirm the required product tests and documentation separately. Manufacturing equipment alone does not certify the finished barrier system.
Request a Quotation
IUWON can assess a suitable configuration based on your intended guardrail products and production targets.
Please provide:
- W-beam, Thrie-beam, or custom profile drawings
- Steel grade, thickness, and coating
- Coil width and maximum coil weight
- Punching layout and finished beam lengths
- Required production output
- Electrical supply and factory layout requirements
With these details, IUWON can evaluate the tooling, drive system, punching and cutting arrangements, and auxiliary equipment required for your project.
Contact IUWON to discuss your guardrail production requirements and request a technical quotation.
Hot Tags: guardrail roll former, China guardrail roll former manufacturers, suppliers, factory